Inquiry Us
Leave Your Message

How to Choose the Right CNC Machine?

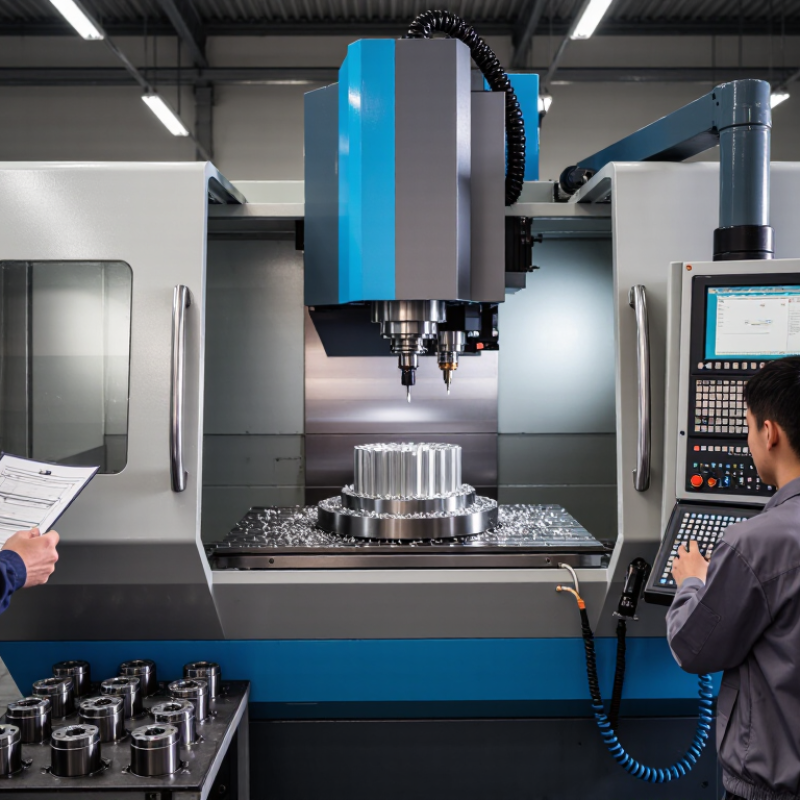
Choosing the right Cnc Machine begins with the workpiece, not the machine’s price tag. A small aluminum bracket needs different capabilities from a hardened steel mold. Material, dimensions, tolerance, surface finish, and production volume should guide the search. A practical evaluation starts with real drawings and sample parts. Marketing brochures can look impressive. Shop-floor evidence matters more. Reviewing cutting tests, spindle performance, and machine stability helps reveal limitations before purchase.

Machine configuration deserves close attention. A three-axis model may suit flat plates and routine drilling. Complex molds often demand four or five axes. Check the working envelope against the largest planned part. Leave enough room for fixtures and tool movement. Spindle speed, torque, rapid motion, and tool capacity affect daily output. Software compatibility also matters. An advanced controller is unhelpful if operators cannot use it confidently. Ask suppliers about training, service response times, spare parts, and documented accuracy tests. Reliable support can prevent a small fault from causing a costly week of downtime.

Budget calculations should include installation, tooling, inspection equipment, energy use, maintenance, and operator training. The cheapest quote may not create the lowest operating cost. A machine that looked ideal on paper may struggle with vibration, chip evacuation, or limited floor space. That possibility deserves honest attention. Speak with experienced machinists and request references from comparable workshops. If possible, inspect a running machine and measure its finished parts. No choice is perfect. The strongest decision balances technical evidence, business goals, and shop-floor realities. This guide explains how to compare those factors with care, practical judgment, and room for revision.

How to Choose the Right CNC Machine?

Define Your CNC Machining Goals and Production Requirements

Choosing the right CNC machine starts with a clear production goal, not a machine catalog. Define the part materials, dimensions, tolerances, surface finish, and expected annual volume. A small aluminum bracket may need a compact three-axis mill. A steel housing with several angled faces may justify four or five axes. Record actual cycle time, setup time, and inspection time from similar jobs. Guessing here can create expensive capacity problems.

Labor also matters. The National Association of Manufacturers’ 2023 survey reported that 72.1% of manufacturers struggled to attract or retain employees. A machine with simpler programming, automatic tool measurement, and reliable probing may reduce dependence on scarce skills. However, automation cannot repair poor process planning. I have seen shops buy advanced equipment before fixing unstable workholding. The result was impressive hardware and disappointing output. A perfect machine rarely exists.

Tips: Build a one-page requirements sheet before requesting quotations. Include spindle speed, work envelope, tooling, coolant needs, tolerance targets, and operator skill levels. Compare the machine’s rated accuracy with your real inspection data. The International Organization for Standardization’s ISO 230-2 standard emphasizes testing positioning accuracy and repeatability under defined conditions. Ask for comparable test results, not vague claims. Also calculate the payback using realistic utilization. The U.S. Bureau of Labor Statistics projects a 3% decline in machinist employment from 2023 to 2033, increasing the value of accessible controls and documented training. Still, I would reserve budget for maintenance, fixtures, and programming time. These costs are easy to overlook.

Compare CNC Machine Types and Their Suitable Applications

Choosing a CNC machine starts with the part, not the machine’s price. A three-axis machining center suits flat plates, pockets, and small fixtures. Add a fourth axis for indexed faces and repeated side drilling. Five-axis machines reach complex impellers, molds, and medical geometries with fewer setups. According to Grand View Research, the global CNC machine market reached about US$83.6 billion in 2023. It is projected to grow through 2030. This growth reflects wider automation, but every machine still has practical limits.

A CNC lathe works well for shafts, bushings, and threaded components. Live tooling can mill flats or cross-holes in one cycle. For sheet metal, CNC laser and plasma systems cut profiles quickly. A press brake handles controlled bends. Routers suit wood, plastics, composites, and some aluminum work. Heavy cutting can expose their weaknesses. The 2024 World Manufacturing Forum report identifies flexibility, digital connectivity, and skilled labor as major manufacturing priorities. Connectivity helps only when operators can maintain it.

Match the machine to tolerances, material hardness, batch size, and floor space. Check spindle power, work envelope, tool capacity, chip evacuation, and service access. A powerful spindle may waste energy on thin aluminum panels. A small lathe may struggle with long, vibration-prone shafts. The boundary is not always clean. Test a real part. Measure cutting time, setup time, scrap, and training needs. These costs can outweigh brochure speed. Some purchasing decisions still rely on incomplete shop data. That is worth admitting.

How to Choose the Right CNC Machine?

Compare CNC machine types by their suitability for common manufacturing applications. A score of 5 indicates an excellent fit, while 1 indicates limited suitability.

Selection guide: CNC lathes are best for rotational parts, milling machines for prismatic components, 5-axis machines for complex surfaces, routers for sheet materials, wire EDM for precise conductive parts, and waterjet machines for heat-sensitive materials.

Evaluate Machine Specifications, Accuracy, Capacity, and Compatibility

Choosing the right CNC machine requires more than comparing price and power. Start with the machine specifications that match your daily work. Check spindle speed, motor power, travel distance, control functions, and tool-changing capacity. A machine rated for heavy cutting may still perform poorly with unsuitable tooling.

Measure accuracy and repeatability separately. Accuracy shows how closely the machine reaches a target position. Repeatability shows whether it returns there consistently. Ask for inspection reports, test-cut results, and maintenance records. Do not trust a single number. Thermal changes, vibration, and operator setup can affect real results. Small details matter.

Capacity must fit both current and future jobs. Confirm the maximum workpiece size, table load, axis travel, and fixture clearance. Leave practical space around the part. A tight setup creates avoidable problems. Compatibility is equally important. Review file formats, software requirements, electrical supply, tooling standards, and network connections. Verify that existing fixtures and measuring equipment will work with the new machine.

A trial cut is valuable. Use a material and tolerance similar to your production work. Inspect surface finish, dimensional stability, chip removal, and setup time. No checklist is perfect. A machine that looks ideal on paper may expose unexpected limits during production. Keep those limits visible before making the purchase.

How to Choose the Right CNC Machine? — Evaluate Machine Specifications, Accuracy, Capacity, and Compatibility

The comparison below uses typical specifications for common CNC machine categories. Actual performance depends on machine construction, tooling, workholding, material, programming, maintenance, and operating conditions.

Evaluation Dimension 3-Axis CNC Milling Machine 5-Axis CNC Machining Center CNC Turning Center CNC Router CNC Wire EDM
Primary Application Prismatic metal parts, plates, brackets, molds, and general production work Complex parts, impellers, aerospace components, medical parts, and reduced-setup machining Rotational components such as shafts, bushings, pins, threads, and turned profiles Large panels, plastics, wood, composites, aluminum sheets, and sign-making materials High-precision conductive parts, fine slots, punches, dies, and intricate profiles
Typical Axes 3 linear axes: X, Y, and Z 3 linear axes plus 2 rotary axes 2 linear axes, commonly X and Z; live tooling may add milling axes 3 linear axes; optional rotary or tangential axis Typically 4 controlled axes for taper and profile work
Typical Working Envelope Approximately 500–1,500 mm in X; 300–700 mm in Y; 400–700 mm in Z Approximately 300–1,000 mm in X; 300–800 mm in Y; 300–800 mm in Z Approximately 200–800 mm maximum turning diameter; 300–1,500 mm between centers Approximately 1,220 × 2,440 mm to 2,000 × 4,000 mm table size Approximately 300–1,000 mm in X; 200–600 mm in Y; 100–300 mm workpiece height
Typical Positioning Accuracy About ±0.005 to ±0.020 mm, depending on machine class and axis travel About ±0.003 to ±0.010 mm for linear positioning; rotary accuracy requires separate verification About ±0.005 to ±0.015 mm for linear positioning About ±0.020 to ±0.100 mm, depending on frame rigidity, drive system, and table size About ±0.002 to ±0.010 mm, with excellent repeatability on suitable conductive materials
Typical Repeatability Approximately ±0.002 to ±0.008 mm Approximately ±0.002 to ±0.005 mm on linear axes Approximately ±0.002 to ±0.006 mm Approximately ±0.010 to ±0.050 mm Approximately ±0.001 to ±0.005 mm
Spindle or Cutting System Typically 6,000–18,000 rpm; metal-cutting torque is more important than speed alone Typically 8,000–24,000 rpm; high-speed or high-torque spindles are available for different materials Typically 2,000–6,000 rpm; chuck size, bar capacity, and turning torque are critical Typically 12,000–24,000 rpm; router-style spindles favor high-speed cutting and smaller tools Electrode wire commonly ranges from approximately 0.10–0.30 mm; cutting is performed by controlled electrical discharge
Material Compatibility Aluminum, steel, stainless steel, brass, titanium, engineering plastics, and composites Aluminum, steel, titanium, nickel alloys, composites, and complex hardened materials with suitable tooling Steel, stainless steel, aluminum, brass, copper, titanium, plastics, and other machinable bar stock Wood, MDF, plastics, foam, acrylic, composites, and light aluminum work Electrically conductive materials only, including hardened steel, carbide, copper, and selected alloys
Maximum Workpiece Considerations Limited by table load, vise or fixture size, spindle clearance, and tool reach Limited by rotary-table diameter, interference between the tool and part, and machine load capacity Limited by maximum swing, spindle bore, chuck capacity, and workpiece length Large sheet capacity is possible, but heavy metal parts may exceed the gantry or vacuum-table limits Limited by tank dimensions, workpiece height, dielectric circulation, and electrical conductivity
Recommended Workpiece Weight Commonly 300–1,500 kg, depending on table size and machine structure Commonly 200–1,200 kg, with rotary-table capacity requiring specific confirmation Commonly 100–1,500 kg between centers; chuck and tailstock limits must be checked Commonly 50–500 kg, depending on gantry design and table construction Commonly 100–1,000 kg, depending on tank and table capacity
Best Accuracy Choice Strong general-purpose accuracy for most 3-axis components Best for maintaining part relationships across multiple angled surfaces Best for precise diameters, concentric features, and threads Suitable for woodworking, plastics, composites, and non-critical light machining Excellent for fine profiles, narrow slots, and hardened conductive materials
Setup Efficiency Good for simple parts; multiple setups may be required for complex surfaces Very high for complex parts because several faces can be machined in one setup Very high for rotational parts and bar-fed production High for large flat sheets and repeated panel work Moderate; threading the wire and workpiece preparation add process time
CAD/CAM Requirement 2.5D or 3D CAM is commonly used; post-processor compatibility must be confirmed Advanced multi-axis CAM and collision simulation are strongly recommended Turning CAM is useful; live-tooling machines may require mill-turn programming 2D, 2.5D, or 3D CAM is commonly sufficient for routing applications Specialized CAM is required for wire paths, taper, skim cuts, and technology settings
Control and File Compatibility Confirm G-code format, post-processor, probing support, tool-table format, and network connectivity Confirm simultaneous 5-axis capability, tool-center-point control, simulation, and rotary-axis calibration Confirm turning cycles, threading cycles, spindle synchronization, and live-tooling functions Confirm common G-code support, controller resolution, vacuum-table control, and CAD/CAM compatibility Confirm dedicated CAM support, wire technology databases, taper programming, and inspection data export
Tooling and Workholding Vise, fixture plate, collets, face mills, end mills, drills, and probing systems Rotary table or trunnion, modular fixtures, collision-safe holders, and shorter tools when possible Chuck, collet, soft jaws, hard jaws, steady rest, tailstock, and turning-tool holders Vacuum table, clamps, spoilboard, router bits, compression cutters, and dust extraction Wire guides, dielectric filtration, workpiece clamps, and conductive-contact fixtures
Production Strength Versatile for prototypes, low-volume work, and general batch production Excellent for complex, high-value parts with fewer setups Excellent for repetitive rotational production and automated bar work Excellent for high-volume sheet processing and nesting applications Strong for precision work, but usually slower than conventional milling for bulk material removal
Typical Operating Cost Factors Cutting tools, coolant, fixtures, spindle maintenance, and electricity Advanced tooling, rotary-axis maintenance, CAM programming, probing, and skilled labor Cutting inserts, chuck and jaw maintenance, bar stock, coolant, and automation Router bits, dust extraction, vacuum-table power, spoilboards, and material waste Wire consumption, dielectric filtration, deionization resin, water treatment, and maintenance
Operator Skill Level Intermediate; requires setup, work offset, tooling, and basic CAM knowledge Advanced; requires multi-axis programming, fixture planning, and collision control Intermediate to advanced; requires knowledge of workholding, turning geometry, and threading Basic to intermediate; material hold-down and toolpath selection are essential Advanced; requires knowledge of electrical discharge parameters, flushing, and wire management
Best Choice When... You need a flexible metal-cutting machine for standard prismatic components You need complex geometry, fewer setups, or improved access to multiple surfaces Your parts are primarily rotational and require accurate diameters or threads You process large sheets or non-ferrous materials and prioritize throughput over heavy cutting You need tight profiles or intricate cuts in hardened, electrically conductive materials
Key Questions Before Purchase Is the spindle powerful enough for the material? Is the table large enough? Is the controller compatible with your CAM system? What are the true simultaneous-axis capabilities? How are rotary accuracy and thermal compensation verified? What are the maximum swing, spindle bore, chuck size, bar capacity, and threading capabilities? Can the gantry handle your material weight? Is vacuum hold-down adequate? Is dust collection included? Does the machine support your material thickness and taper requirements? What are wire and dielectric costs?

Selection rule: Match the machine to the dominant material, part geometry, dimensional tolerance, workpiece size, production volume, available floor space, operator skill, and CAD/CAM workflow. Always verify final specifications using standardized acceptance tests, such as positioning accuracy and repeatability measurements under the applicable machine-tool standard.

Assess Software, Automation, Maintenance, and Operator Requirements

How to Choose the Right CNC Machine?

Assess Software, Automation, Maintenance, and Operator Requirements

The software should match your production reality, not just the machine’s brochure. Check file compatibility, postprocessor accuracy, simulation tools, and update procedures. A reliable system shows tool paths clearly and flags collisions before cutting begins. Ask whether operators can edit offsets without opening complex menus. Small delays become expensive during repeated production. Test the software with one of your actual parts.

Automation can improve output, but it also adds responsibility. Consider pallet changers, bar feeders, probing systems, and automatic tool measurement. These features reduce handling time when parts are consistent. They may create frustration when your jobs change daily. I once saw a highly automated setup slow down because workers lacked clear recovery instructions. The lesson is uncomfortable: automation does not replace training. It changes the training.

Maintenance requirements deserve equal attention. Review lubrication points, filter access, diagnostic messages, and recommended inspection intervals. A machine that is easy to service usually returns to production faster. Ask who performs routine checks and who handles technical faults. Operators need practical training, not a one-hour demonstration. Keep cleaning tools, checklists, and spare wear parts nearby. Even experienced teams miss details when maintenance records are vague. That weakness should influence the final choice.

Calculate Total Cost, Support Services, and Long-Term Value

How to Choose the Right CNC Machine?

Calculate Total Cost, Support Services, and Long-Term Value

Choosing a CNC machine starts with more than its purchase price. Calculate total cost before comparing specifications. Include tooling, installation, training, software, electricity, maintenance, and financing fees. A machine priced lower may require expensive upgrades later. Ask for a written estimate with clear assumptions. Some costs are easily missed.

Support becomes important when production stops unexpectedly. Check response times, technician availability, spare-part access, and remote diagnostic options. Request references from companies with similar workloads. I would also test the training process before signing an agreement. Clear manuals help, but practical instruction matters more. Support should not disappear after installation.

Long-term value depends on useful output, not impressive specifications. Estimate annual production, acceptable cycle times, expected accuracy, and future material requirements. Then compare that gain with maintenance and downtime risks. A flexible machine can handle changing orders and reduce future replacement costs. Resale value may matter, but it should not control the decision. Forecasts are rarely perfect. Leave room for mistakes. Choose capacity you can support, not capacity you merely admire.