Inquiry Us
Leave Your Message

10 Tips for Buying a Horizontal Machining Center?

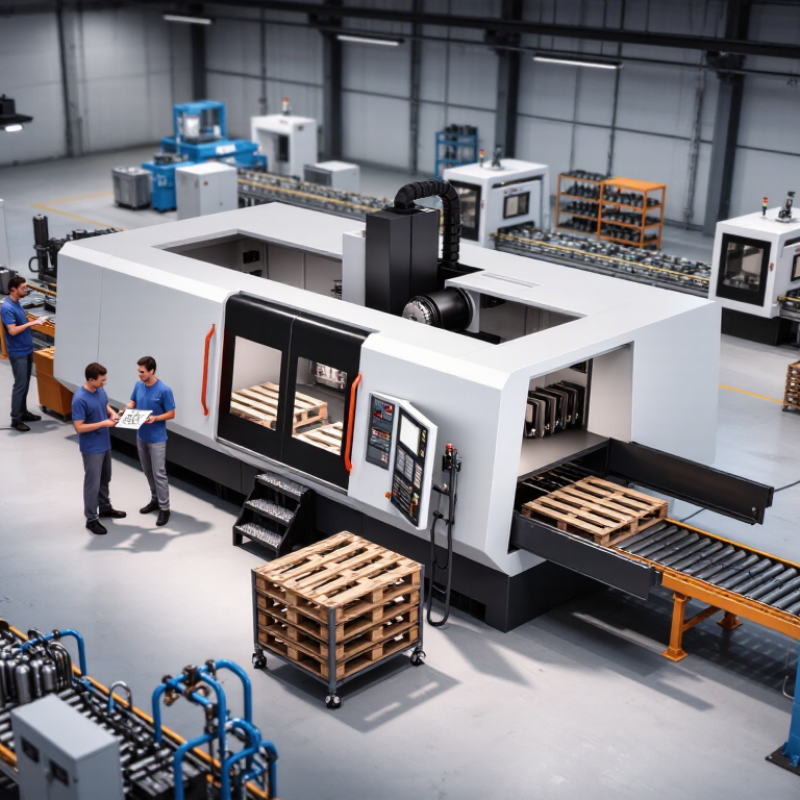
Buying a Horizontal Machining Center is not a spindle-speed contest. It is a decision about throughput, part quality, labor, and the work your shop expects to run. A fourth pallet, for example, may reduce changeover delays, but it only pays off when your production schedule can use it. Details matter.

The 2024 Deloitte–Manufacturing Institute talent study projects that U.S. manufacturing may need 3.8 million additional workers by 2033, with 1.9 million jobs potentially unfilled. That forecast is not a machine-tool sales report, but it highlights why staffing, automation, and ease of operation belong in a buying decision. A faster machine is not automatically the better choice.

Manufacturing-systems expert Eliyahu Goldratt wrote, “An hour lost at a bottleneck is an hour lost for the entire system.” For a Horizontal Machining Center, that idea makes cycle time only one part of the calculation. Look closely at spindle uptime, tool capacity, pallet-change time, chip evacuation, service response, and operator training. Ask suppliers to demonstrate your actual part, not a convenient sample. Then compare the complete installed cost with realistic production gains. This guide covers ten practical checks, from machine configuration to support after installation. Some estimates will be imperfect; record the assumptions, and revisit them before signing. A small overlooked detail can become an expensive daily problem.

10 Tips for Buying a Horizontal Machining Center?

Define Part Size, Pallet Load, and 4-Sided Access Before Comparing Machines

A horizontal machining center should fit the part and its workholding, not just the part drawing. Measure the largest component, including features that overhang a fixture or tombstone. Leave room for cutting tools to reach deep pockets without striking clamps. Measure twice. A few extra millimeters can change the setup.

Tip: Calculate pallet load with the fixture, tombstone, clamps, and workpiece included. Check the machine’s rated load and how weight is distributed; an off-center setup may behave differently from a balanced one. Also confirm the part’s center of gravity and loading method. A heavy fixture can consume capacity before the workpiece reaches the pallet.

Four-sided access can reduce repositioning, but it depends on real tool clearance around the part. Sketch the tool approach for each side, then check for collisions with clamps, neighboring parts, and the machine enclosure. Ask whether common tools can reach all required faces in one setup. That sounds obvious, yet it is easy to overlook when comparing travel specifications alone. Leave room. I would also review a representative setup with an experienced programmer or operator before choosing; shop assumptions are not always right. The best comparison uses your actual part, pallet load, and fixture layout—not a maximum-size claim.

Match 40- or 50-Taper Spindles to Tooling, Torque, and Cutting Loads

A 40-taper spindle can suit fast, frequent tool changes and moderate cutting loads. Its lighter tooling may help a machine accelerate quickly, especially when producing many smaller parts. But speed alone does not guarantee productivity. Check the spindle’s torque curve, not just its maximum RPM.

A 50-taper spindle usually supports heavier tools and greater rigidity under demanding cuts. That can matter when roughing steel, using a long boring bar, or removing substantial material from a large casting. Feel the difference in the numbers: compare torque at the RPM your cutter actually needs. A high peak torque figure may exist only at low speed. Tool length, holder mass, and workpiece setup also affect stability.

Match the taper to your real tool inventory and the cuts that consume the most machine time. Ask suppliers for continuous torque data, allowable tool weight, and spindle acceleration details. Then review the figures against your longest tools and heaviest planned cuts. There is a catch: a larger taper can add cost and mass without improving light-duty work. I would question any choice based only on “more rigid.” It is an easy assumption, and sometimes the wrong one. A short test cut with your intended tooling can expose vibration or power limits before purchase.

10 Tips for Buying a Horizontal Machining Center: Match 40- or 50-Taper Spindles to Tooling, Torque, and Cutting Loads

Use these points as a comparison guide, not as fixed spindle specifications. Speed, torque, power, tool capacity, and cutting performance vary by machine configuration; confirm the published performance curves and limits for the exact model.

Tip Decision Area What to Check 40-Taper Considerations 50-Taper Considerations Practical Buying Action
1 Start with the cutting load Define the materials, typical stock allowance, tool diameters, depth of cut, and expected production rate. These factors determine the torque and rigidity actually needed. Often a good fit for lighter-to-moderate cutting loads, smaller tools, and applications where faster spindle response is useful. Often preferred for heavier cuts, larger tools, or demanding roughing where increased tool-interface rigidity is valuable. Bring representative part drawings and cutting data to the supplier. Request a machining test using your material and intended tooling.
2 Match the tool interface Check the exact taper standard and retention method, such as CAT, BT, or a specified HSK interface. These interfaces and their components are not automatically interchangeable. Confirm the exact 40-taper interface, pull-stud specification where applicable, and toolholder balance requirements. Confirm the exact 50-taper interface and retention hardware. Do not assume that holders from another taper standard will fit. Specify the interface in the purchase document and verify that existing holders, pull studs, and presetting equipment are compatible.
3 Compare torque across the working range Request a spindle torque-versus-speed curve. Peak torque at low rpm does not show how much torque remains at the speeds used for cutting. A 40-taper machine can provide substantial torque, but the available torque depends on its motor, gearing, and spindle design. A 50-taper machine is commonly selected for higher-load work, but the taper alone does not guarantee a particular torque value. Compare continuous and peak torque at your actual cutting rpm, and check how long peak torque is available.
4 Read power and torque together Power and torque are related by speed: torque (N·m) ≈ 9,550 × power (kW) ÷ speed (rpm). For example, 30 kW at 3,000 rpm corresponds to about 95.5 N·m. High maximum rpm can suit smaller tools and faster cutting, but maximum power may only be available over part of the speed range. Low-speed torque can be important for large cutters and heavy roughing; verify the curve rather than relying on a peak-power headline. Ask for both the power and torque curves, including continuous ratings, and compare them at the speeds used for your cuts.
5 Choose speed for the actual tools Calculate cutting speed from tool diameter and rpm. Maximum spindle speed is useful only when the workpiece, cutter, holder, and setup can safely use it. Many 40-taper configurations are aimed at higher-speed work, though available speed ranges vary substantially by design. Many conventional 50-taper configurations prioritize stiffness and torque at lower speeds; high-speed 50-taper options also exist. List the diameter and required rpm of your most-used cutters. Confirm the spindle’s continuous operating range and tool-system speed limits.
6 Check tool mass and reach Long, heavy tools increase bending and vibration risk. Toolholder length, cutter projection, balance, and tool mass all affect practical cutting capability. Check the machine’s tool-mass and tool-length limits carefully, especially for long-reach or heavy assemblies. A larger taper may support more demanding tool assemblies, but actual limits are set by the spindle, holder, changer, and machine specifications. Provide the heaviest and longest planned tool assemblies for review. Verify automatic tool-change limits as well as spindle limits.
7 Assess rigidity beyond the taper Machine structure, spindle bearings, column, rotary table, fixture, toolholder, and workpiece all contribute to system rigidity. A 40-taper setup may perform well on demanding work when the complete machine, holder, and fixture are appropriately sized. A 50-taper interface can be advantageous for heavy cutting, but it cannot compensate for a flexible machine or poor workholding. Evaluate the complete load path and request a test cut. Compare surface finish, tool wear, and stability under your intended conditions.
8 Verify chip and coolant capacity Heavy material removal generates chips and heat. Check through-spindle coolant pressure and flow, filtration, chip conveyors, and enclosure capacity. Suitable for many high-speed and moderate-load processes when coolant delivery and chip evacuation match the operation. Heavy roughing may create larger chip volumes and higher thermal loads; confirm the coolant and conveyor package is sized accordingly. Ask for coolant flow and pressure at the tool, filtration details, and chip-conveyor capacity for the materials you machine.
9 Review spindle duty and thermal behavior Continuous cutting, frequent acceleration, and extended high-speed operation create different thermal demands. Peak ratings may not be continuous ratings. For sustained high-speed work, check thermal growth, warm-up requirements, and the spindle’s continuous speed rating. For sustained high-torque cutting, check continuous torque, bearing limits, and cooling performance under load. Request continuous-duty data and clarify any time limits on peak power, peak torque, or maximum speed.
10 Compare total operating cost Include tooling inventory, holder availability, tool-change time, maintenance, energy use, and the cost of adapting existing processes. May be economical when compatible holders are already in use and the application does not require a heavier interface. May justify its cost when heavier tools or cutting loads improve throughput or reduce process limitations. Compare the complete package and run a representative production trial. Select the spindle that meets the required process window, not just the largest rating.

Compare Axis Positioning Accuracy and Repeatability Using ISO 230-2

When buying a horizontal machining center, compare axis positioning accuracy and repeatability under the same test conditions. ISO 230-2:2014, the international machine-tool test code, defines how to assess positioning performance on numerically controlled axes. Its reported measures include positioning deviations and repeatability in both travel directions. Ask for the actual test results, not just a single “accuracy” figure. A tidy number can hide variation.

Check the test length, target positions, approach direction, and measurement conditions. For example, an axis may return consistently to a point yet show a directional offset when approached from the other side. That distinction matters when boring a row of holes across a large fixture. ISO 230-2 results are useful for comparison, but they do not automatically predict performance under cutting loads, coolant, or a warm shop. Ask whether the acceptance report records these limits and measurement uncertainty.

Then compare machines using matching travel ranges and methods. Small differences matter. And a test sheet may still leave questions.

Source: ISO 230-2:2014, Test code for machine tools—Determination of accuracy and repeatability of positioning of numerically controlled axes.

Assess Finished-Part Accuracy with ISO 10791-7 Test Pieces

When comparing horizontal machining centers, ask for an ISO 10791-7 test-piece report, not just a positioning-accuracy figure. The standard evaluates accuracy on a machined test piece, bringing cutting performance into view. That matters. A machine can meet an axis specification yet produce different results under real cutting loads.

Check what was actually tested. Request the test-piece drawing, measured results, material, cutting conditions, tool details, and machine configuration. Look closely at reported dimensions and geometric features, such as hole locations and relationships between machined surfaces. Confirm how the part was measured and whether measurement uncertainty is stated. Small differences can matter when a part has tight tolerances.

A test piece is evidence, not a promise. Ask whether the result reflects the machine’s current setup, including thermal state, fixture, and tool condition. If possible, witness a repeat test or have an independent metrology specialist inspect the piece. Compare results with your own part requirements, rather than treating one passing sample as proof of every production outcome. That conclusion would be too generous. Some details, like workholding stiffness or long-run temperature changes, may need separate trials.

10 Tips for Buying a Horizontal Machining Center

Assess Finished-Part Accuracy with ISO 10791-7 Test Pieces

Example readings show deviations from nominal for selected machined features; they are illustrative, not ISO acceptance limits or results from a specific machine. When comparing machines, inspect an appropriate test piece using the acceptance criteria for the applicable ISO 10791-7 edition, and consider measurement uncertainty and the test conditions.

Estimate Pallet-Changer Payback from Cycle Time and Shift Hours

A pallet changer can reduce the time a horizontal machining center sits idle between jobs. To estimate payback, compare the machine time recovered with the changer’s installed cost. Start with actual cycle times, not the fastest cycle from a sales estimate.

If a part runs for 42 minutes and loading takes 8 minutes, the operator may handle the next pallet while the spindle cuts. That overlap is the opportunity.

It does not guarantee more output if inspection, tooling, or material supply already limits production.

Count realistic shift hours and planned production days. Suppose the changer saves 6 minutes per cycle across 30 cycles per shift. That is 3 recovered hours per shift, before accounting for breaks, stoppages, and schedule gaps.

Be cautious. Convert only usable hours into value, using the contribution earned per productive machine hour, then compare that annual benefit with the changer’s purchase and installation cost. Divide the cost by the annual benefit for a simple payback estimate.

For example, a $90,000 investment and $45,000 in verified yearly benefit imply about two years.

The estimate will be imperfect. Track several weeks of load times and downtime before deciding; a neat spreadsheet can still miss a fixture delay or an operator pulled onto another task.